
Optimized Automix catalogue with exact verified photos where available and clean photo spaces for pending images.
3 product rows
0 exact photos
49 product rows
12 exact photos
19 product rows
0 exact photos
14 product rows
0 exact photos
8 product rows
0 exact photos
70 product rows
16 exact photos
19 product rows
0 exact photos
5 product rows
0 exact photos
32 product rows
2 exact photos
Turning insert family for CNC turning applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| CNMA120404 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMA120408 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMA120412 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
80° diamond negative inserts for rough turning, forged components and interrupted machining.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| CNMG120404-CQ | CQ | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| CNMG120404-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
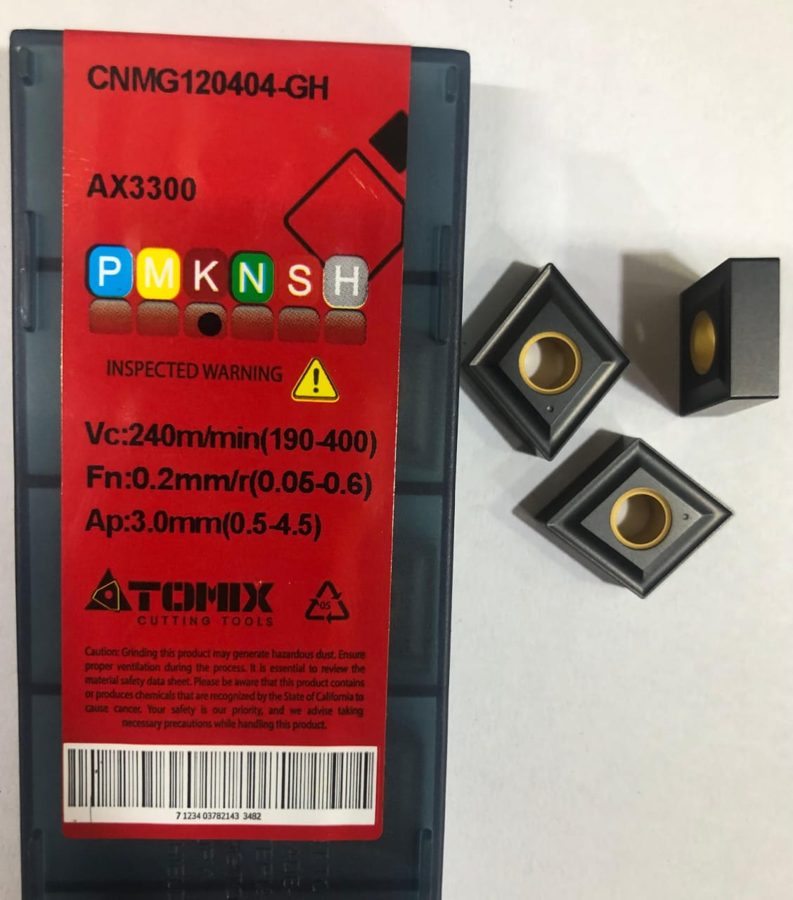
| CNMG120404-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120404-MQ | MQ | AX3200 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120404-MQ | MQ | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120404-EM | EM | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-PM | PM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120404-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-45 | 45 | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-CQ | CQ | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-EM | EM | AX3200 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-EM | EM | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-EM | EM | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| CNMG120408-GH | GH | AX3350 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| CNMG120408-HQ | HQ | AX3125C | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-LM | LM | AX3200 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-MA | MA | AX3200S | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-MQ | MQ | AX3200S | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120408-MQ | MQ | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120408-MS | MS | AX3200 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120408-MS | MS | AX3200S | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120408-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| CNMG120408-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-PM | PM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-TM | TM | AX3150D | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120408-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120412 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120412-CQ | CQ | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120412-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| CNMG120412-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120412-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120412-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG120412-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG190612-GR | GR | AX3150 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| CNMG190612-PM | PM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG190616-PM | PM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| CNMG190616-QR | QR | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
55° negative diamond inserts for profile turning and medium roughing.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| DNMG110404-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| DNMG110408-FG | FG | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150604-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150604-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150604-PM | PM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150604-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150604-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150604-VL | VL | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150608-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150608-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150608-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| DNMG150608-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150608-PM | PM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150608-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150608-VL | VL | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150612-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150612-PM | PM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150612-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| DNMG150612-VL | VL | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Square negative inserts with multiple cutting edges for economical roughing and facing.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SNMG120404-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120404-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120404-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120408 | Standard | AX3350 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120408-MA | MA | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120408-MA | MA | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120408-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120408-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120408-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG120408-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG190612-GR | GR | AX3150 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| SNMG190612-PM | PM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG190616-PM | PM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| SNMG190616-QR | QR | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Turning insert family for CNC turning applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TNMA160404 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMA160404 | Standard | AX3350 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMA160408 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMA160408 | Standard | AX3350 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMA160412 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMA160412 | Standard | AX3350 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMA160404-4 | 4 | OPD100 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMA160408-4 | 4 | OPD100 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Triangular negative double-sided turning inserts for external turning, facing and production machining.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TNMG160404-CQ | CQ | AX3125 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-CQ | CQ | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-EA | EA | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-EM | EM | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-HQ | HQ | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404L | Standard | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404L-ZC | ZC | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404L-ZC | ZC | AX3150D | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-MA | MA | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-MQ | MQ | AX3200 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| TNMG160404-MQ | MQ | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| TNMG160404-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| TNMG160404-MSF | MSF | AX3200 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| TNMG160404-PC | PC | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-PM | PM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-PM | PM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404R | Standard | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404R-90 | 90 | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404R-ZC | ZC | AX3125A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404R-ZC | ZC | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160404-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-CQ | CQ | AX3105 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-CQ | CQ | AX3125 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-CQ | CQ | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-EM | EM | AX3200 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-EM | EM | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-HQ | HQ | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| TNMG160408L | Standard | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408L-ZC | ZC | AX3105 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408L-ZC | ZC | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408L-ZC | ZC | AX3200 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-GH | GH | AX3350 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| TNMG160408-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-MQ | MQ | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| TNMG160408-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| TNMG160408-MS | MS | AX3200 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| TNMG160408-PC | PC | AX3125 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-PC | PC | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-PM | PM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-PM | PM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408R | Standard | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408R-ZC | ZC | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-TM | TM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160408-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-43 | 43 | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-CQ | CQ | AX3125 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-CQ | CQ | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-CQ | CQ | AX3150D | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| TNMG160412-GH | GH | AX3350 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| TNMG160412-HQ | HQ | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-MA | MA | AX3200 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-PC | PC | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-PM | PM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-TM | TM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| TNMG160412-TM | TM | AX3150B | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
35° negative V-shape inserts for profiling, contour turning and finishing.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| VNMG12T304 | Standard | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG12T304 | Standard | AX3105 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG12T304 | Standard | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG12T308 | Standard | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG12T304-LIM | LIM | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG12T308-LIM | LIM | AX3150 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160404-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160404-MQ | MQ | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| VNMG160404-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| VNMG160404-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160408-PM | PM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160404-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160408-TM | TM | AX3105 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160404-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160408-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160408-MQ | MQ | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| VNMG160408-MS | MS | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| VNMG160408-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| VNMG160412-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Turning insert family for CNC turning applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| WNMA080404 | Standard | AX3350 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMA080408 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMA080408 | Standard | AX3350 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMA080412 | Standard | AX3300 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMA080412 | Standard | AX3350 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
80° trigon negative inserts for rough turning, facing and stable production machining.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| WNMG060408-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080404-EM | EM | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080404-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| WNMG080404-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080404-MQ | MQ | AX3220 | Stainless / chip-control medium turning | Stainless steel / steel | 100–240 m/min | 0.08–0.35 mm/rev | 0.3–4.0 mm |
| WNMG080404-PM | PM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080404-PM | PM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080404-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-EM | EM | AX3200 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-EM | EM | AX3220 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-FG | FG | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| WNMG080408-GH | GH | AX3350 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| WNMG080408-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-MT | MT | AX3125 | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-PC | PC | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-PM | PM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-PM | PM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-TM | TM | AX3150B | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080408-TM | TM | AX3150C | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-GH | GH | AX3300 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| WNMG080412-GH | GH | AX3350 | Heavy roughing and interrupted cutting | Steel / alloy steel / forging | 100–260 m/min | 0.20–0.75 mm/rev | 1.0–8.0 mm |
| WNMG080412-PM | PM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-PM | PM | AX3125A | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-MA | MA | AX3220 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-PC | PC | AX3220A | OD turning, facing and production turning | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-TM | TM | AX3125 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-TM | TM | AX3125B | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-TM | TM | AX3150 | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
| WNMG080412-TM | TM | AX3150B | Medium turning and semi-roughing | Steel / alloy steel / forging | 140–320 m/min | 0.10–0.55 mm/rev | 0.3–6.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
66 product rows
7 exact photos
47 product rows
10 exact photos
5 product rows
0 exact photos
39 product rows
9 exact photos
6 product rows
0 exact photos
3 product rows
0 exact photos
24 product rows
9 exact photos
Positive 80° diamond inserts for boring bars, internal turning and finishing.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| CCMT060202-MS | MS | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-EM | EM | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-EM | EM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-FG | FG | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060204-FG | FG | AX3220A | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060204-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-MSL | MSL | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-TPC | TPC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060204-SL1 | SL1 | AX3125 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060204-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060204-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060204-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060204-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060204-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060208-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060208-MSL | MSL | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060208-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT060208-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060208-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060208-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060208-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT060208-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T302-FM | FM | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T302-FM | FM | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T302-FM | FM | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T302-SM | SM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-53 | 53 | AX3125A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-53 | 53 | AX3105 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-53 | 53 | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-EM | EM | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-FG | FG | AX3220A | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T304-HM | HM | AX3105 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-HM | HM | AX3300 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-HQ | HQ | AX3105 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-MQ | MQ | AX3200S | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-MQ | MQ | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-MSL | MSL | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T304-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T304-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T304-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T304-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T304-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T304-WSM | WSM | AX3350 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308-EM | EM | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308-FG | FG | AX3220A | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T308-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308-HM | HM | AX3300 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308 HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308-MF | MF | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308-MSL | MSL | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT09T308-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T308-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T308-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T308-SL1 | SL1 | AX3350 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT09T308-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| CCMT120404-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT120404-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT120408-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT120408-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| CCMT120408-SL1 | SL1 | AX3350 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Positive 55° diamond inserts for profiling, taper turning and light boring.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| DCMT070202-MV | MV | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070202-MV | MV | AX3200 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070202-MV | MV | AX3200S | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070202-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070204-FG | FG | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070204-FG | FG | AX3220A | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070204-HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070204-MQ | MQ | AX3200S | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070204-MV | MV | AX3200S | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070204-MV | MV | AX3200 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070204-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070204-SL1 | SL1 | AX3125 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070204-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070204-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070204-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070204-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070204-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT070208-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT070208-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T302-MV | MV | AX3105 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T302-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T304-FG | FG | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T304-FG | FG | AX3220A | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T304-FM | FM | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T304-MQ | MQ | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T304-MQ | MQ | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T304-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T304-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T304-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T304-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T304-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T304-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-FG | FG | AX3220A | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T308-HQ | HQ | AX3125C | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-MV | MV | AX3125 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-MV | MV | AX3200 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-MV | MV | AX3200S | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T308-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T308-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| DCMT11T308-TM | TM | AX3150 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-WM | WM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| DCMT11T308-WM | WM | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Positive square inserts for boring, facing and stable finishing operations.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SCMT09T308-HM | HM | AX3105 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| SCMT09T308-HM | HM | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| SCMT09T308-HQ | HQ | AX3105 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| SCMT09T308-HQ | HQ | AX3125C | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| SCMT09T308-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Positive triangular inserts for light turning, boring and finishing.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TCMT090204-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT090204-FM | FM | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT090204-FM | FM | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT090208-TM | TM | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110202-24 | 24 | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110202-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110202-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110204-FG | FG | AX3220A | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110204-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110204-MSL | MSL | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110204-SL1 | SL1 | AX3105 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110204-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110204-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110204-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110204-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110204-SL1 | SL1 | AX3350 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110208-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110208-MSL | MSL | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110208-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110208-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110208-SL1 | SL1 | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110208-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT110208-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110208-HQ | HQ | AX3125C | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT110208-HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T304-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T304-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T304-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT16T304-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT16T308-HM | HM | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T308-HM | HM | AX3300 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T308-OTF | OTF | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T308-PC | PC | AX3220A | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T308-SL1 | SL1 | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT16T308-SL1 | SL1 | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT16T308-SL1 | SL1 | AX3300 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| TCMT16T308-TM | TM | AX3105 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT16T308-TM | TM | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TCMT220408-OTR | OTR | AX3200 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Boring, profiling or positive turning insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TPGH080202L | Standard | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TPGH080204L | Standard | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TPGH090202L | Standard | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TPGH090204L | Standard | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TPGH110302L | Standard | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TPGH110304L | Standard | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Boring, profiling or positive turning insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TPMH090204-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TPMH110304-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| TPMH110308-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Positive V-shape inserts for fine boring, profiling and low cutting force machining.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| VBMT110302-FM | FM | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| VBMT110302-FM | FM | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| VBMT110302-FM | FM | AX3200S | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| VBMT110302-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110304-FM | FM | AX3200 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| VBMT110304-FM | FM | AX3220 | Fine finishing and low cutting force boring | Steel / stainless / alloy steel | 140–320 m/min | 0.04–0.22 mm/rev | 0.05–2.0 mm |
| VBMT110304-HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110304-MV | MV | AX3125 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110304-MV | MV | AX3200 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110304-MV | MV | AX3200S | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110304-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110308-HQ | HQ | AX3125C | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110308-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110308-MV | MV | AX3300 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT110308-MV | MV | AX3200S | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160404-HQ | HQ | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160404-MV | MV | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160404-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160404-WM | WM | AX3150 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160404-WM | WM | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160408-MV | MV | AX3150 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160408-MV | MV | AX3220 | Profiling, boring and semi-finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160408-WM | WM | AX3150 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
| VBMT160408-WM | WM | AX3220 | Boring, profiling and finishing | Steel / stainless / alloy steel | 120–300 m/min | 0.04–0.30 mm/rev | 0.05–3.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
4 product rows
0 exact photos
1 product rows
0 exact photos
1 product rows
0 exact photos
20 product rows
0 exact photos
3 product rows
0 exact photos
1 product rows
0 exact photos
1 product rows
0 exact photos
2 product rows
0 exact photos
2 product rows
0 exact photos
2 product rows
0 exact photos
2 product rows
0 exact photos
4 product rows
0 exact photos
5 product rows
0 exact photos
2 product rows
0 exact photos
11 product rows
0 exact photos
1 product rows
0 exact photos
6 product rows
0 exact photos
9 product rows
6 exact photos
1 product rows
0 exact photos
2 product rows
0 exact photos
2 product rows
0 exact photos
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 3PKT100408R | Standard | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| 3PKT100404R | Standard | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| 3PKT100408R | Standard | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| 3PKT150508R | Standard | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| ADMT070204 | Standard | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Parallelogram milling inserts for shoulder and side milling.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| APKT160408-PM | PM | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Parallelogram milling inserts for shoulder milling, slot milling and VMC production.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| APMT1135PDER-DU | DU | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-DU | DU | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-DU | DU | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-H2 | H2 | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-H2 | H2 | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-H2 | H2 | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-H2 | H2 | AX3220B | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-M2 | M2 | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-M2 | M2 | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-M2 | M2 | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-M2 | M2 | AX3220C | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1135PDER-SD | SD | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-DU | DU | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-H2 | H2 | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-H2 | H2 | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-H2 | H2 | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-M2 | M2 | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-M2 | M2 | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-M2 | M2 | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMT1604PDER-SDX | SDX | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| APMW113504-4.5 | 4.5 | OPD100 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMW180404-5 | 5 | OPD100 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| APMW180408-5 | 5 | OPD100 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| BDMT11T316ER-JT | JT | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| EPMT0603TN-8-1 | 1 | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| JDMT100308R-FW | FW | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| JDMT150508R | Standard | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| LNMU0303ZER-MJ | MJ | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| LNMU0303ZER-MJ | MJ | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| LOGU030310ER | Standard | AX3220A | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| LOGU030310ER | Standard | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| ONMU080608 | Standard | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| ONMU080608 | Standard | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| RDKW10T3MO-BG | BG | AX3200 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDKW10T3MO-BG | BG | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDKW1204MO-BG | BG | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDKW1605MO-BG | BG | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| RDKX1204MO-BG | BG | AX3200 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDKX1204MO-BG | BG | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDKX10T3MO QBG | QBG | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDKX1605MO | Standard | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDKX1605MO | Standard | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| RDMW0803MO-D | D | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RDMW10T3MO-D | D | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| RPMT08T2MOE | Standard | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT08T2MOE-JS | JS | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT08T2MOE-JS | JS | AX3200 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT08T2MOE-JS | JS | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT10T3MOE-JS | JS | AX3200 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT10T3MOE-JS | JS | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT10T3MOE-JS | JS | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT1204MO-DU | DU | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT1204MO-DU | DU | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT1204MOE-JS | JS | AX3200 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| RPMT1204MOE-JS | JS | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SDMT120512-GM | GM | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SNMX1206ANN-MMK | MMK | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SNMX1206ANN-MMK | MMK | AX3300 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SNMX1206ANN-MMK | MMK | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SNMX1206QNN | Standard | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SNMX1206QNN-MMK | MMK | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SNMX1206QNN-MMK | MMK | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Square milling inserts for face milling and high-feed milling.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SOMT050204-DP | DP | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT060204-DP | DP | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT070306-DP | DP | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT08T306-DP | DP | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT09T308-DP | DP | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT11T308-DP | DP | AX3220 | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT11T308-DP | DP | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT130408-DP | DP | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| SOMT150510-DP | DP | AX3220A | Face milling, profile milling or high-feed milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TPKN2204PDTR-Q1 | Q1 | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TPKR2204PDTR | Standard | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| TPKR2204PDTR | Standard | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Milling insert family for VMC and machining centre applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| WNMU080608EN-GM | GM | AX3220 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
| WNMU080608EN-GM | GM | AX3200 | VMC milling, shoulder milling and face milling | Steel / alloy steel / cast iron | 120–280 m/min | 0.08–0.40 mm/tooth | 0.3–5.0 mm |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
6 product rows
0 exact photos
6 product rows
0 exact photos
10 product rows
0 exact photos
8 product rows
0 exact photos
23 product rows
6 exact photos
9 product rows
0 exact photos
11 product rows
0 exact photos
2 product rows
0 exact photos
2 product rows
0 exact photos
1 product rows
0 exact photos
2 product rows
0 exact photos
3 product rows
0 exact photos
1 product rows
0 exact photos
4 product rows
0 exact photos
1 product rows
0 exact photos
2 product rows
0 exact photos
2 product rows
0 exact photos
2 product rows
0 exact photos
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 6GR-100 | 100 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 6GR-100 | 100 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 6GR-150 | 150 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 6GR-150 | 150 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 6GR-200 | 200 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 6GR-200 | 200 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 7GR-100 | 100 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 7GR-100 | 100 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 7GR-150 | 150 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 7GR-150 | 150 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 7GR-200 | 200 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 7GR-200 | 200 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 8GR-100 | 100 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-100 | 100 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-150 | 150 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-150 | 150 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-200 | 200 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-200 | 200 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-250 | 250 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-250 | 250 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-300 | 300 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 8GR-300 | 300 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 9GR-100 | 100 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 9GR-100 | 100 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 9GR-150 | 150 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 9GR-150 | 150 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 9GR-200 | 200 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 9GR-250 | 250 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 9GR-250 | 250 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| 9GR-300 | 300 | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving and parting inserts for G/M/T geometry grooving applications.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| MGMN150-G | G | AX3200 | Sharp finishing groove and low-force grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN150-G | G | AX3220 | Sharp finishing groove and low-force grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN200-G | G | AX3200 | Sharp finishing groove and low-force grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN200-T | T | AX3200 | Tough heavy-duty grooving / interrupted cuts | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN200-T | T | AX3220 | Tough heavy-duty grooving / interrupted cuts | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN200-G | G | AX3220 | Sharp finishing groove and low-force grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN250-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN250-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN250-G | G | AX3220 | Sharp finishing groove and low-force grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN250-G | G | AX3200 | Sharp finishing groove and low-force grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN300-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN300-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN300-T | T | AX3200 | Tough heavy-duty grooving / interrupted cuts | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN300-T | T | AX3220 | Tough heavy-duty grooving / interrupted cuts | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN400-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN400-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN400-T | T | AX3200 | Tough heavy-duty grooving / interrupted cuts | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN400-T | T | AX3220 | Tough heavy-duty grooving / interrupted cuts | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN500-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN500-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN500-T | T | AX3220 | Tough heavy-duty grooving / interrupted cuts | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN600-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MGMN600-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Round / multi-groove style grooving inserts for deep groove work.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| MRMN200-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN200-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN200-M | M | AX3450 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN300-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN300-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN400-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN400-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN500-M | M | AX3200 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| MRMN500-M | M | AX3220 | Universal medium grooving | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Penta-style grooving inserts for multiple-edge grooving and parting.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| PENTA 24N050J | 24N050J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N050J | 24N050J | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N080J | 24N080J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N100J | 24N100J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N100J | 24N100J | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N120J | 24N120J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N150J | 24N150J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N200J | 24N200J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N200J | 24N200J | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N250J | 24N250J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| PENTA 24N300J | 24N300J | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDC2 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDC2 | Standard | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDC3 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDC3 | Standard | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDC4 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDJ2 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDJ2 | Standard | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDJ3 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDJ3 | Standard | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDJ3 | Standard | AX3220A | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDJ4 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDKU-200 | 200 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDKU-300 | 300 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDKU-400 | 400 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDKU-500 | 500 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDT 2E-1.0-RU(TDR2) | RU(TDR2) | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDT 3E-1.5-RU(TDR3) | RU(TDR3) | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDT3 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDT 4E-2.0-RU(TDR4) | RU(TDR4) | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDT4 | Standard | AX3200 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Grooving, parting or cutoff insert family.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| TDXU3E-0.3 | 0.3 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
| TDXU4E-0.4 | 0.4 | AX3220 | Grooving, parting and cutoff operation | Steel / stainless / alloy steel | 60–190 m/min | 0.03–0.18 mm/rev | Width based |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
6 product rows
0 exact photos
41 product rows
0 exact photos
40 product rows
1 exact photos
45 product rows
0 exact photos
62 product rows
1 exact photos
Small internal threading inserts.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 11IR/EL0.8 | EL0.8 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 11IR/EL0.8 | EL0.8 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 11IR/EL1.0 | EL1.0 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 11IR/EL1.0 | EL1.0 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 11IR/EL1.5 | EL1.5 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 11IR/EL1.5 | EL1.5 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
External threading inserts for metric threading.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 16ER/IL0.5 | IL0.5 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.5 | IL0.5 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.6 | IL0.6 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.6 | IL0.6 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.7 | IL0.7 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.7 | IL0.7 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.8 | IL0.8 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.8 | IL0.8 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.9 | IL0.9 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL0.9 | IL0.9 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.0 | IL1.0 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.0 | IL1.0 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.1 | IL1.1 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.2 | IL1.2 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.2 | IL1.2 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.3 | IL1.3 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.3 | IL1.3 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.4 | IL1.4 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.5 | IL1.5 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.6 | IL1.6 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.7 | IL1.7 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.7 | IL1.7 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.75 | IL1.75 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.8 | IL1.8 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.85 | IL1.85 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.85 | IL1.85 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL1.9 | IL1.9 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.0 | IL2.0 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.1 | IL2.1 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.15 | IL2.15 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.2 | IL2.2 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.25 | IL2.25 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.25 | IL2.25 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.3 | IL2.3 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.4 | IL2.4 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.5 | IL2.5 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.6 | IL2.6 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.7 | IL2.7 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.8 | IL2.8 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL2.9 | IL2.9 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16ER/IL3.0 | IL3.0 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Internal threading inserts for metric threading.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| 16IR/EL0.5 | EL0.5 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.5 | EL0.5 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.6 | EL0.6 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.6 | EL0.6 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.7 | EL0.7 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.7 | EL0.7 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.8 | EL0.8 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.8 | EL0.8 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.9 | EL0.9 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL0.9 | EL0.9 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.0 | EL1.0 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.1 | EL1.1 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.2 | EL1.2 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.2 | EL1.2 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.3 | EL1.3 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.4 | EL1.4 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.5 | EL1.5 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.6 | EL1.6 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.6 | EL1.6 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.7 | EL1.7 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.75 | EL1.75 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.75 | EL1.75 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.8 | EL1.8 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.85 | EL1.85 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.85 | EL1.85 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL1.9 | EL1.9 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.0 | EL2.0 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.1 | EL2.1 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.15 | EL2.15 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.2 | EL2.2 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.25 | EL2.25 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.25 | EL2.25 | AX3220 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.3 | EL2.3 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.4 | EL2.4 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.5 | EL2.5 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.6 | EL2.6 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.7 | EL2.7 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.8 | EL2.8 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL2.9 | EL2.9 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| 16IR/EL3.0 | EL3.0 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
External threading insert family for ISO, NPT, BSPT, UN and special threads.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| ER/RT11601G-8ACME | ACME | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-11BSPTM | BSPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-14BSPTM | BSPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-8NPTM | NPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-18NPTM | NPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-11.5NPT | NPT | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-14NPT | NPT | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-8UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-14UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-16UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-18UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-20UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-24UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-8WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-9WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-10W | Thread profile | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-11WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-12WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-14WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-16WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-18WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-19WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-20WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-24WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-26WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-32WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-100ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-125ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-150ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-175ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-200ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-200ISOM | ISOM | AX3220A | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-250ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-300ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-300ISOM | ISOM | AX3220A | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-350ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-AG55M | AG55M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT11601G-AG60M | AG60M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT2201G-400ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT2201G-450ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT2201G-500ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT2201G-550ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT2201G-600ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT2201G-N55M | N55M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| ER/RT2201G-N60M | N60M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Internal threading insert family for ISO, NPT, BSPT and special threads.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| IR/RT0601L-100ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT0601L-150ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT0601L-A55 | A55 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT0601L-A60 | A60 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT0801L-100ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT0801L-150ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT0801L-A55 | A55 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT0801L-A60M | A60 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-14WA | Thread profile | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-100ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-125ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-150ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-200ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-250ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-A55 | A55 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1101L-A60 | A60 | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-8ACME-YT | ACME | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-11BSPTM | BSPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-14BSPTM | BSPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-8NPTM | NPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-11.5NPT | NPT | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-14NPT | NPT | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-18NPTM | NPTM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-8UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-16UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-18UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-20UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-24UNM | UNM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-8WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-9WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-10WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-11WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-12WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-14WA | Thread profile | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-14WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-16WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-18WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-19W | Thread profile | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-20WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-24WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-26WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-32WM | WM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-100ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-125ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1 1601L-175ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1 1601L-150ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1601L-150ISOM | ISOM | AX3220A | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1 1601L-200ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1601L-200ISOM | ISOM | AX3220A | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1 1601L-250ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1601L-250ISOM | ISOM | AX3220A | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1 1601L-300ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT11601L-350ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1 1601L-AG55M | AG55M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT1 1601L-AG60M | AG60M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT2201L-400ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT2201L-450ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT2201L-500ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT2201L-550ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT2201L-600ISOM | ISOM | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT2201L-N55M | N55M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
| IR/RT2201L-N60M | N60M | AX3200 | CNC thread cutting | Steel / stainless / alloy steel | 40–120 m/min | Pitch based | Multi-pass cycle |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
8 product rows
0 exact photos
12 product rows
8 exact photos
2 product rows
0 exact photos
5 product rows
2 exact photos
8 product rows
0 exact photos
Positive drill inserts for precision drilling and light cutting.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SPGT050204-PM | PM | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPGT050204-PM | PM | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPGT060204-PM | PM | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPGT07T308-PM | PM | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPGT090408-PM | PM | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPGT110408-PM | PM | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPGT110408-PM | PM | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPGT140512-PM | PM | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Square drill inserts for indexable U-drill and production hole-making.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SPMG050204-DG | DG | AX3220A | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG050204-DG | DG | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG060204-DG | DG | AX3220A | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG060204-DG | DG | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG07T308-DG | DG | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG07T308-DG | DG | AX3220A | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG090408-DG | DG | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG090408-DG | DG | AX3220A | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG110408-DG | DG | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG110408-DG | DG | AX3220A | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG140512-DG | DG | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMG140512-DG | DG | AX3220A | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
Drilling insert family for indexable drilling systems.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| SPMT040204-PD | PD | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| SPMT040204-PD | PD | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
WCMT style drill inserts for indexable drilling systems.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| WCMT050308FN | Standard | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMT050308FN | Standard | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMT06T308FN | Standard | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMT06T308FN | Standard | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMT080412FN | Standard | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.
WCMX drill inserts for replaceable insert drill systems.
Original family image shown once. Product variants and technical data are listed below without repeated images or pricing.
| Part Name / Description | Geometry | Grade | Usage | Material | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|---|---|
| WCMX030208-ZK | ZK | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMX040208FN | Standard | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMX040208FN | Standard | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMX040208-ZK | ZK | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMX040208-ZK | ZK | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMX06T308-ZK | ZK | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMX080412B-ZK | ZK | AX3200 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
| WCMX080412B-ZK | ZK | AX3220 | Indexable drilling and U-drill hole making | Steel / cast iron | 100–220 m/min | 0.05–0.20 mm/rev | Drilling operation |
Cutting parameters shown are retained from the existing technical catalogue data. Confirm final values for material, grade, rigidity and coolant conditions before production use.